What Type of MIG Hard Surfacing Wire Is Best?

Time:2026-09-24 Author:Sophia
0%

Choosing the right Mig Hard Surfacing Wire starts with understanding what the part actually faces. A conveyor roller worn by dry abrasion needs a different deposit from a bucket edge struck by rock. The wire must suit the wear mechanism, the base metal, and the welding process. A high-alloy deposit may resist abrasion well, yet crack under repeated impact. There is no universal best choice.

This guide compares common wire options and the conditions they serve. It explains how alloy content, hardness, and deposit structure affect service life. It also considers practical details: wire-feed stability, bead shape, dilution, and preheat requirements. Small differences matter. A bead that looks smooth on a test plate can behave differently on a thick, cold component. Manufacturer data sheets and a qualified procedure are useful starting points, not guarantees. Results still depend on preparation and technique.

Before selecting a wire, identify the dominant wear, check the component material, and review operating temperatures. Then compare product recommendations against the real job. Some claims sound convincing. Verify them with test welds or field data when possible. This is not always easy, and the first selection may need adjustment. The goal is a compatible, dependable deposit—not simply the hardest one.
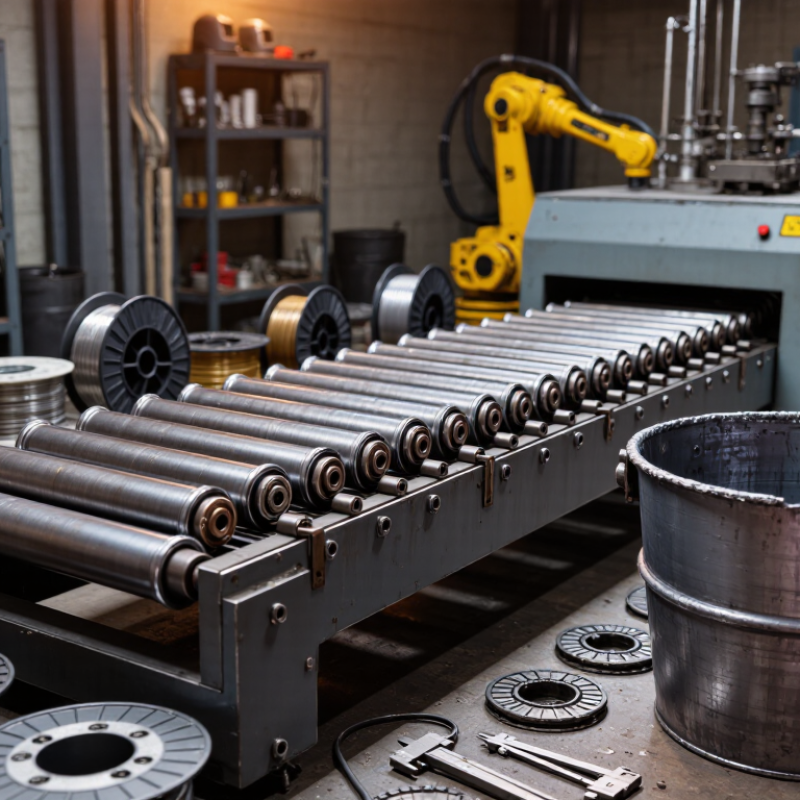
What Type of MIG Hard Surfacing Wire Is Best?

What MIG Hard Surfacing Wire Is and How It Works

What Type of MIG Hard Surfacing Wire Is Best?

What MIG Hard Surfacing Wire Is and How It Works

MIG hard surfacing wire deposits a wear-resistant alloy onto a steel surface using a continuously fed electrode and shielding gas. The base metal melts slightly, while the wire forms an overlay that resists abrasion, impact, or metal-to-metal wear. Think of a loader bucket edge: the overlay takes much of the scraping, while the underlying steel supports the load. AWS’s Welding Handbook describes hardfacing as a way to restore or protect components, but the right deposit depends on the wear mechanism. A chromium-carbide overlay may suit severe abrasion; a tougher, lower-hardness alloy may better tolerate impact. Typical chromium-carbide deposits can reach roughly 55–65 HRC, though actual hardness varies with wire chemistry and welding conditions. Harder is not always better.

The process is sensitive to heat input, travel speed, and bead placement. Excessive heat can dilute the overlay with base metal, reducing its intended properties. ASTM G65 provides a dry-sand/rubber-wheel abrasion test; its reported volume loss helps compare materials under controlled conditions, not predict every field result. Real service includes changing loads, dirt, and operator technique. I would treat lab rankings as a starting point, not a promise.

Tips: Clean oil and scale from the workpiece, then check the wire’s recommended polarity, gas, and preheat. Run a small test bead and inspect for cracking or excessive dilution. Keep records. They help, even when the first trial is imperfect.

The Main Types of MIG Hard Surfacing Wire

The main MIG hard-surfacing wire types differ in how they handle abrasion, impact, and heat. Chromium-carbide wires suit severe sliding abrasion, such as sand moving through a chute. Their hard carbide particles resist wear, but the deposit can crack under heavy impact. Martensitic wires offer a tougher balance for loader buckets and crusher parts. They are less abrasion-resistant than carbide-rich deposits, yet tolerate knocks better.

Cobalt-based wires retain hardness at elevated temperatures and resist metal-to-metal wear. They are useful on hot valves or tooling, but usually cost more and are not the default choice for cold, abrasive service. Tool-steel wires provide another option where edge retention matters. AWS Welding Handbook guidance describes hardfacing alloy families by wear conditions; reported deposit hardness commonly spans roughly 20–65 HRC, depending on chemistry and procedure. That range is broad. Hardness alone can mislead.

Wire format matters too. Solid wires often produce a smoother, more controlled bead, while metal-cored wires can increase deposition rate and support alloy-rich deposits. AWS A5.21 classifies hardfacing electrodes by composition and deposit characteristics, helping buyers compare wires beyond trade descriptions. Check the classification, dilution limits, and recommended number of layers. A polished coupon may look sound, yet a thick overlay can still crack in service. Test on a representative part when failure is costly.

How Wire Composition Affects Wear Resistance and Toughness

The best MIG hard surfacing wire depends on what the part actually encounters. For gritty sliding wear, a deposit rich in chromium carbides can resist abrasion because hard particles shield the softer metal around them. More carbide is not automatically better. A highly wear-resistant layer may crack under repeated impact or bending.

Carbon and chromium levels influence carbide formation, hardness, and the deposit’s response to service conditions. Higher carbon can increase hardness, but it may also reduce toughness. Manganese and other alloying elements affect weld-metal strength and behavior, though their effect depends on the complete wire chemistry. Match the composition to the wear pattern: a conveyor screw handling sand needs a different balance than a crusher part struck by rocks. Small details matter.

Look closely at the base metal, too. Dilution from the underlying steel changes the chemistry of the first layer, so the finished surface may differ from a wire’s stated composition. Check the manufacturer’s technical data for deposit hardness, recommended layers, and any preheat guidance. Then compare those values with actual service conditions, not just a hardness number. I have seen selection discussions focus too narrowly on abrasion; that is an easy mistake. If impact is significant, a slightly softer, tougher deposit may last longer. The right choice is a tradeoff, best confirmed through a controlled trial on the part or a representative sample.

Key Factors for Choosing MIG Hard Surfacing Wire

What Type of MIG Hard Surfacing Wire Is Best?

Key Factors for Choosing MIG Hard Surfacing Wire

The best wire depends on what wears the part: abrasion, impact, or metal-to-metal friction. For a loader bucket cutting edge scraping gritty soil, abrasion resistance may matter most. A crusher component hit by large rocks also needs toughness; an extremely hard deposit can crack under repeated impact. Match the alloy to the wear mechanism, base metal, and repair conditions—not hardness alone.

ASM Handbook guidance describes chromium-carbide overlays as typically reaching about 55–65 HRC, depending on composition and measurement. That range suits severe abrasion, but it does not guarantee longer service life under impact. Also check wire diameter, shielding gas, polarity, and the welding procedure. These affect bead shape, fusion, and dilution, which can change deposit properties. A small test bead on the actual base material is useful. I have seen specifications treat hardness as the whole story; that is an easy shortcut, and sometimes a costly one.

Tips: Compare the wire’s technical data sheet with the part’s operating conditions. Record hardness, crack pattern, and wear after a trial. If the overlay chips at the edges, consider a tougher alloy or a different bead pattern before choosing a harder wire.

Matching Wire Type to the Application and Operating Conditions

What Type of MIG Hard Surfacing Wire Is Best?
Matching Wire Type to the Application and Operating Conditions

The best wire depends on what is wearing the part. For sliding metal contact, a martensitic deposit can offer a useful balance of hardness and impact resistance. For repeated contact with sand or ore, chromium-carbide deposits are often considered; ASM Handbook, Volume 18, reports typical overlay hardness in the 55–65 HRC range. Hardness alone is not a selection rule. A brittle deposit may crack when a bucket edge strikes rock, while a softer layer may wear quickly under steady abrasion.

Check the actual operating conditions: impact, abrasive size, corrosion, temperature, and base-metal chemistry. AWS welding guidance emphasizes controlling heat input and dilution, since the base metal can change the deposited layer’s properties. On a thin steel edge, excessive heat may cause distortion; on a thick component, inadequate fusion can leave a weak bond. Match wire diameter and transfer mode to the machine, joint position, and required bead profile. Then test a sample under representative service conditions. It is easy to overvalue a catalogue hardness figure. Field wear rarely follows a tidy table, and a small trial may reveal a better compromise.

FAQS

What is MIG hard surfacing wire used for?

It adds a wear-resistant layer to a working surface. Common examples include bucket edges, chutes, crusher parts, valves, and tooling.

Which wire suits severe sliding abrasion?

Chromium-carbide wire often suits sand, ore, and other sliding materials. Its hard carbide particles resist wear. Heavy impacts may cause cracking.

When is martensitic wire a better choice?

Martensitic wire offers a useful balance between hardness and toughness. It can suit loader buckets and crusher parts facing repeated knocks. Not perfect for every surface.

Where can cobalt-based wire be useful?

Cobalt-based wire keeps its hardness at elevated temperatures. It may suit hot valves and tooling exposed to metal-to-metal wear. It usually costs more.

Why consider tool-steel wire?

Tool-steel wire can help retain a sharp working edge. It may suit cutting edges and tooling. The result depends strongly on procedure and base metal.

Is the hardest wire always the best option?

No. A very hard deposit may crack when a bucket edge strikes rock. A softer layer may wear faster under steady sand abrasion. Hardness alone misleads.

How do solid and metal-cored wires differ?

Solid wires often create a smoother, more controlled bead. Metal-cored wires can increase deposition rate and support alloy-rich deposits. The machine must handle the selected format.

What operating conditions should guide wire selection?

Check impact, abrasive size, corrosion, temperature, and base-metal chemistry. Also consider bead profile, wire diameter, position, and transfer mode. Small details matter.

Why should a sample be tested before full repair?

A polished test coupon may look sound, yet a thick overlay can crack later. Test a representative part under realistic service conditions. Field wear is rarely tidy.

Conclusion

Mig Hard Surfacing Wire is used to deposit a durable layer of metal onto a component’s surface, helping it resist wear while preserving the underlying part. Different wire types are designed for different conditions, with composition playing a central role in performance. Harder alloys can offer stronger resistance to abrasion, while tougher formulations may better withstand impact or repeated stress. Choosing a wire therefore involves balancing wear resistance with the risk of cracking or damage during service.

The right option depends on the material being repaired or protected, the welding process, and the conditions the component will face. Consider the type of wear, operating temperature, impact level, and whether the part must maintain a particular shape or finish. Matching wire composition and properties to the application can improve service life and avoid selecting a deposit that is either too brittle or insufficiently resistant to wear.
Sophia

Sophia

Sophia is a dedicated marketing professional with an exceptional depth of knowledge about her company's products and services. With a keen understanding of market trends and customer needs, she crafts insightful blog posts that not only inform but also engage readers, enriching the company’s online......